


Maintaining food freshness during international transportation has become one of the biggest challenges for global food brands. Whether exporting snacks, coffee, pet food, frozen foods, or nutritional products, choosing the right barrier film often determines whether products arrive in perfect condition—or lose quality before reaching consumers.
På Huiyang Emballage, we specialize in manufacturing specialfremstillede fleksible plastemballageposer and designing high-performance barrier film structures for food brands worldwide. As a professional flexible packaging manufacturer with over 20 years of experience, we help customers optimize packaging performance, extend shelf life, and reduce transportation risks through advanced material engineering rather than simply increasing film thickness.
This case study explains what barrier film is, why it matters, and how our engineering team helped a snack food exporter significantly improve product shelf life by upgrading its packaging structure.
What Is Barrier Film?
Many buyers ask:
What is Barrier Film?
Barrier film is not a single material. Instead, it refers to a category of packaging films specifically engineered to block oxygen, moisture, light, aroma, and other external contaminants.
The primary purpose of barrier film is to preserve product freshness, extend shelf life, and protect food quality during storage and transportation.
A barrier film can be made from one or several high-performance materials depending on the required protection level.
Common Barrier Film materials include:
| Barrier Film Material | Hovedfunktion |
|---|---|
| Aluminum Foil (AL) | Outstanding oxygen, moisture and light barrier |
| EVOH | Fremragende iltbarriere |
| Metallized PET (VMPET) | High barrier with lower cost than aluminum |
| BOPA (nylon) | Puncture resistance and mechanical strength |
| PVDC | Excellent gas barrier |
| SiOx / AlOx PET | Transparent high barrier solutions |
| High Barrier PE | Recyclable barrier packaging applications |
Rather than relying on one material, professional manufacturers combine multiple layers to build customized Barrier Film structures for different products.
Why Barrier Film Is Essential for Export Food Packaging
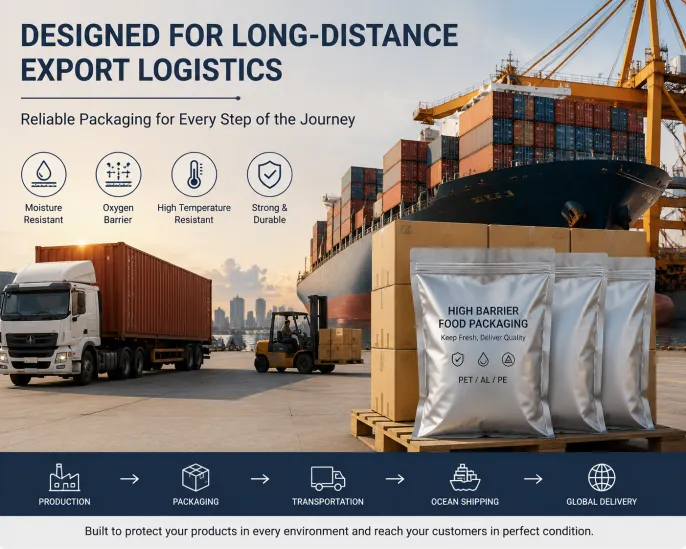
Domestic transportation may only require products to remain fresh for a few weeks.
Export packaging faces much harsher conditions.
Products may experience:
- Long ocean transportation
- High humidity
- Large temperature fluctuations
- Container condensation
- Extended warehouse storage
- Retail shelf display
Without sufficient Barrier Film, oxygen and moisture gradually penetrate the package, causing:
- Loss of crispness
- Oxidation
- Flavor deterioration
- Reduced shelf life
- Higher customer complaints
This is why selecting the proper Barrier Film for food packaging is critical for international brands.
Kundens baggrund
One of Huiyang Emballage‘s customers is a mid-sized snack manufacturer located in Southeast Asia.
Their products include:
- Dried fruit snacks
- Baked vegetable chips
- Healthy snack products
Primary export markets included:
- Middle East
- Europe
- International retail chains
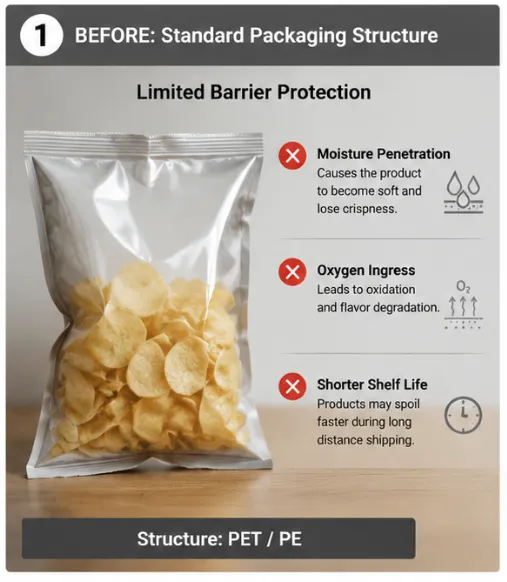
Their original packaging used a standard laminate:
PET / PE
This structure worked well for domestic sales but proved insufficient for long-distance export logistics.
The Packaging Problems
Several months after expanding into export markets, the client encountered multiple quality issues.
1. Shelf Life Became Much Shorter
Products expected to remain fresh for 6–8 months showed noticeable quality decline after only 3–4 months.
2. Moisture Entered the Package
The snacks gradually lost their crisp texture because the original packaging lacked sufficient moisture protection.
3. Flavor and Aroma Declined
Consumers reported inconsistent taste and reduced aroma after products reached overseas retailers.
Engineering Analysis by Huiyang Emballage
Our technical team conducted material testing and packaging analysis.
The results showed that the existing PET/PE laminate provided limited protection against:
- Oxygen
- Moisture
- Light
For export environments involving high humidity and elevated temperatures, the original packaging simply did not provide enough barrier performance.
The issue was not packaging thickness.
The real problem was the barrier film structure.
Our Barrier Film Solution
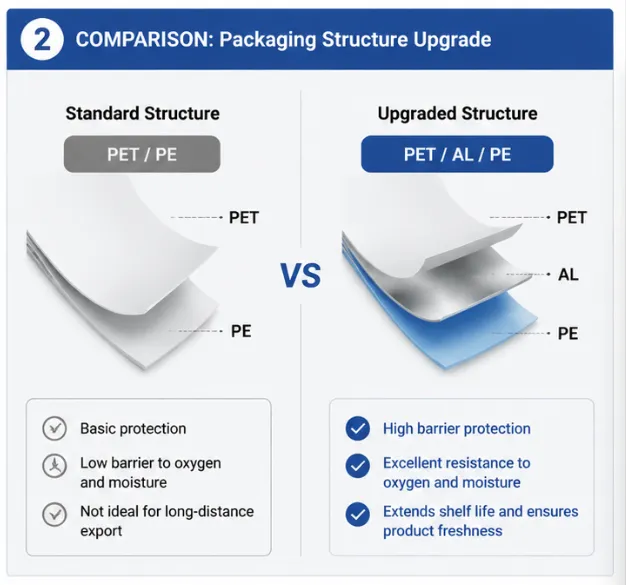
Instead of increasing film thickness, Huiyang Emballage redesigned the material structure using a customized high barrier film system.
Final Packaging Structure
PET / AL / PE
This optimized barrier film offered dramatically improved protection.
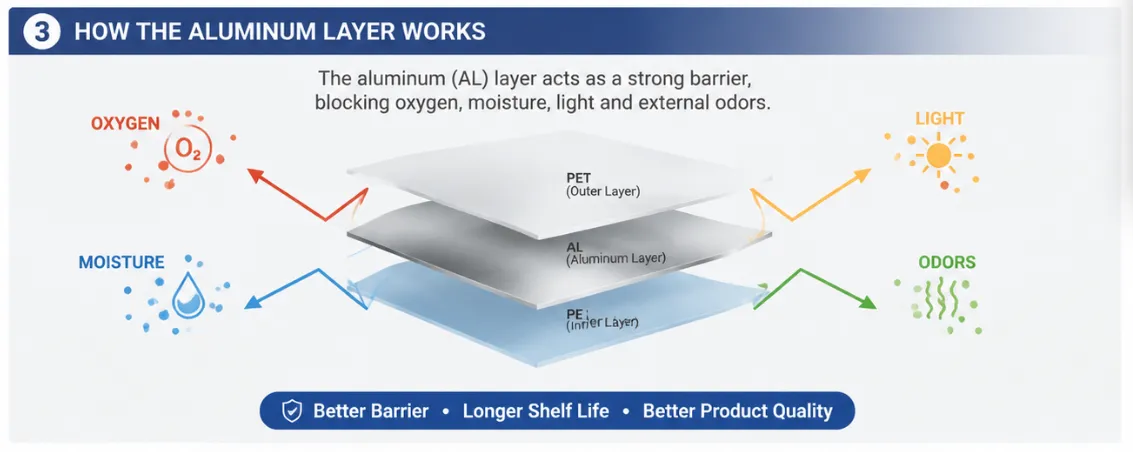
1. Aluminum Barrier Layer
The aluminum foil layer became the core of the new barrier film.
Benefits included:
- Outstanding oxygen barrier
- Excellent moisture resistance
- Superior light protection
- Reduced oxidation
This significantly extended product freshness.
2. Improved Heat Seal Performance
Our engineers optimized:
- Heat sealing temperature
- Sealing pressure
- Sealant layer design
The stronger seals prevented air leakage during transportation.
3. Optimized Film Thickness
Rather than using unnecessarily thick films, we carefully balanced:
- Protection
- Material cost
- Machine efficiency
- Transportation durability
This reduced overall packaging costs while improving performance.
4. Export Simulation Testing
Before mass production, Huiyang Emballage performed simulated transportation testing.
Testing conditions included:
- High humidity
- High temperature
- Long transportation periods
These conditions closely matched Middle East shipping routes.
The customized Barrier Film successfully maintained package integrity throughout testing.
Results After Upgrading to High Barrier Film
Following implementation of the new barrier film structure, the client achieved measurable improvements.
| Performance | Before | After |
|---|---|---|
| Holdbarhed | 3–4 Months | 7–8 Months |
| Moisture Damage | Frequent | Reduced by Over 80% |
| Flavor Retention | Moderate | Significantly Improved |
| Customer Complaints | Høj | Sharp Reduction |
| Retail Reorders | Stable | Noticeable Increase |
The improved packaging enabled the customer to successfully enter additional European retail chains.
How to Choose the Right Barrier Film for Food Packaging
Different foods require different Barrier Film structures.
| Food Product | Recommended Barrier Film Structure |
|---|---|
| Kaffe | PET / AL / PE |
| Te | PET / VMPET / PE |
| Snacks | PET / AL / PE |
| Frozen Foods | PET / NY / PE |
| Saucer | PET / AL / CPP |
| Foder til kæledyr | PET / NY / PE |
| Powder Products | PET / EVOH / PE |
Selecting the proper Barrier Film should consider:
- Produktets egenskaber
- Shelf-life goals
- Transportbetingelser
- Påfyldningsproces
- Target export markets
Hvorfor fødevaremærker vælger Huiyang Emballage
As a professional manufacturer of custom flexible plastic packaging bags, Huiyang Emballage provides complete packaging engineering solutions—not just packaging production.
Our factory advantages include:
- Over 20 års erfaring med fremstilling af fleksibel emballage
- Advanced gravure printing and digital printing technologies
- Professional barrier film engineering team
- OEM & ODM custom packaging services
- Produktionssystemer, der er certificeret til fødevarebrug
- High-barrier laminated film manufacturing
- Streng kvalitetskontrol gennem hele produktionsforløbet
- Fast production and stable global delivery
- Support for low MOQ and large-volume orders
- Extensive export experience serving customers worldwide
From material selection to structural optimization, our engineers help customers reduce costs while maximizing product protection.
Ofte stillede spørgsmål
Is Barrier Film a specific material?
Nej. Barrier film refers to a category of packaging materials designed to prevent oxygen, moisture, and light from entering the package. It can include aluminum foil, EVOH, VMPET, PVDC, SiOx PET, BOPA, and other specialized materials.
What is the best Barrier Film for food packaging?
There is no universal solution. The best barrier film depends on your product, shelf-life requirements, transportation environment, and budget.
Does thicker packaging always provide better barrier performance?
Not necessarily.
A well-designed multi-layer barrier film often delivers significantly better protection than a much thicker single-layer film.
Konklusion
At vælge det rigtige barrier film is one of the most effective ways to improve food shelf life, reduce product waste, and enhance customer satisfaction in international markets. Rather than relying solely on thicker packaging, successful food brands invest in scientifically engineered barrier film structures that provide the optimal balance of protection, efficiency, and cost.
På Huiyang Emballage, we specialize in designing and manufacturing specialfremstillede fleksible plastemballageposer with advanced barrier film solutions tailored to each customer’s product, filling process, and export destination. From material selection and structure optimization to OEM/ODM production and quality control, our experienced engineering team helps global food brands build packaging that protects products and supports long-term business growth.
Looking for the right barrier film for your food products? Contact Huiyang Emballage today for a free packaging consultation and discover how our customized high-barrier flexible packaging solutions can extend shelf life, improve export performance, and strengthen your brand in global markets.